Additive manufacturing (AM) is a manufacturing technology used for 3D object production which opens a pathway to fabricate complex parts due to the high geometrical flexibility of the technology [1]. Direct Metal Laser Sintering (DMLS) is one of the most widely applied metal AM technologies, where, in a layer-by-layer fashion, bulk parts are created by selective sintering and consolidation of thin powder layers using a laser beam [2]. DMLS can be used for part fabrication using different metals and their alloys. Although iron and its alloys have been used in conventional manufacturing for a long time and the most advantages and disadvantages of these materials are well known, using them in additive manufacturing to achieve high quality still can be problematic. In DMLS, the main challenge is to understand the influence of energy density on porosity, microstructure and mechanical properties of a manufactured part.
In this study, test specimens were produced from 17-4PH stainless steel using different sets of build parameters on the EOSINT M280 machine. Cross-sectional microstructure of the manufactured specimens was investigated using scanning electron microscopy (SEM) and optical microscopy in order to determine the relation between porosity and energy density applied during the printing process. Defects visible in cross-sections were evaluated with help of image processing software, which showed the amount of pores present in specimens, depending on various energy density values.
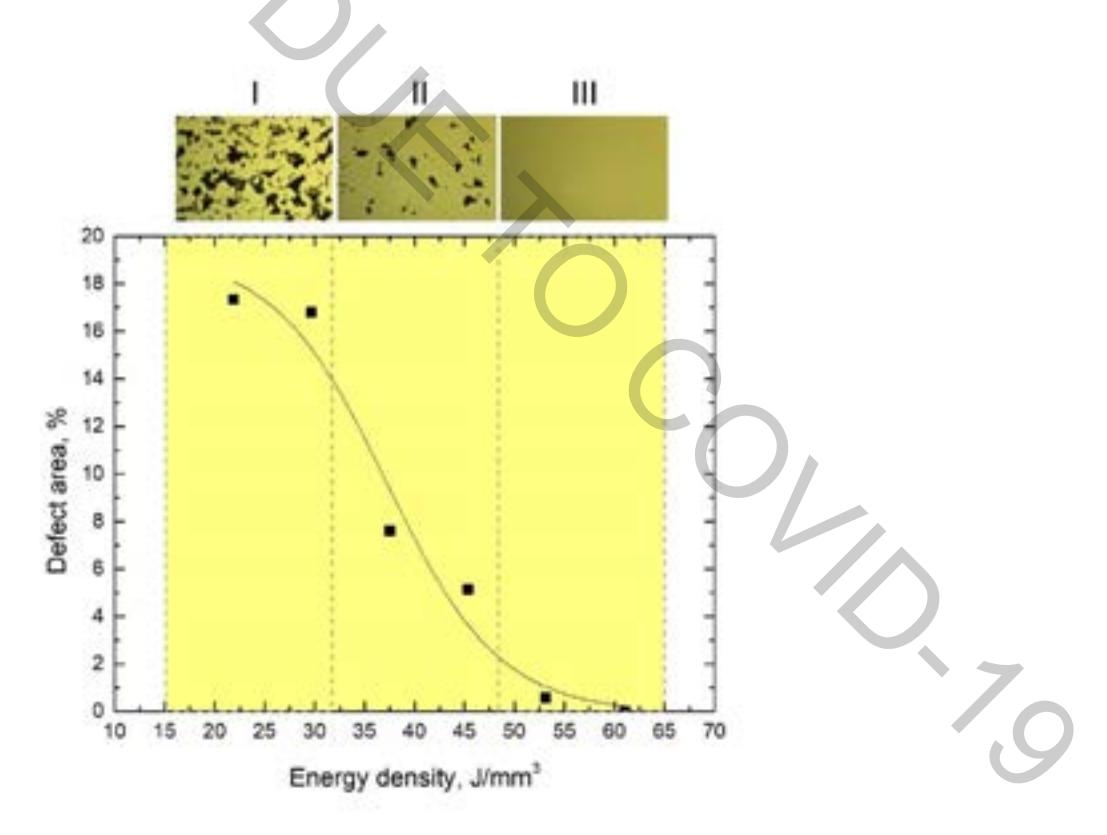
Energy density values vary throughout the experiment and there is a visible decrease in the amount of defects, the higher the energy density is. All manufactured stainless steel parts could be divided into three different types depending on their cross-sectional microstructure: 15-32 J/mm3 (I), 32-48 J/mm3 (II) and 48-65 J/mm3 (III), The zones and optical micrographs corresponding to each of them are shown in Fig.1. All defects compiled take up 16,5-17,5% of the area in I, 5-7% in II and less than 0,5% in III.